Explore cutting-edge articles on laboratory products, industry innovations, and research trends with Lab Consulting.
Choosing the right Cnc Cutting Tools is not a catalog exercise. It is a production decision that affects cycle time, surface finish, tool life, and scrap risk. The Grand View Research report on the global CNC machine market estimated its value at $101.22 billion in 2023 and projected a 9.8% compound annual growth rate from 2024 to 2030. That figure describes CNC machines, not cutting tools, but it signals a growing machining environment where tool selection matters. A busy shop floor makes the consequences visible: chipped edges, heat-darkened chips, and a spindle waiting while an operator changes a tool.
Start with the material, operation, machine, and production goal. A carbide end mill suited to aluminum may not perform well in stainless steel. Coating, geometry, flute count, and tool-holder rigidity all influence results. So does coolant delivery. Professor Tony Schmitz, a machining researcher at the University of Tennessee, studies the dynamics behind cutting processes. His work supports a useful selection principle: evaluate the tool as part of the complete machining system, rather than in isolation. Check the machine’s power and speed limits, then compare supplier data with a controlled shop test.
Small details matter. A few microns of runout can shorten tool life. Measure the first part. Inspect the chips. Record wear and cycle time. Then adjust.
This guide explains how to compare tool materials, coatings, geometries, and costs. It also highlights common selection mistakes, so buyers can make decisions based on verified performance—not a promising label alone.
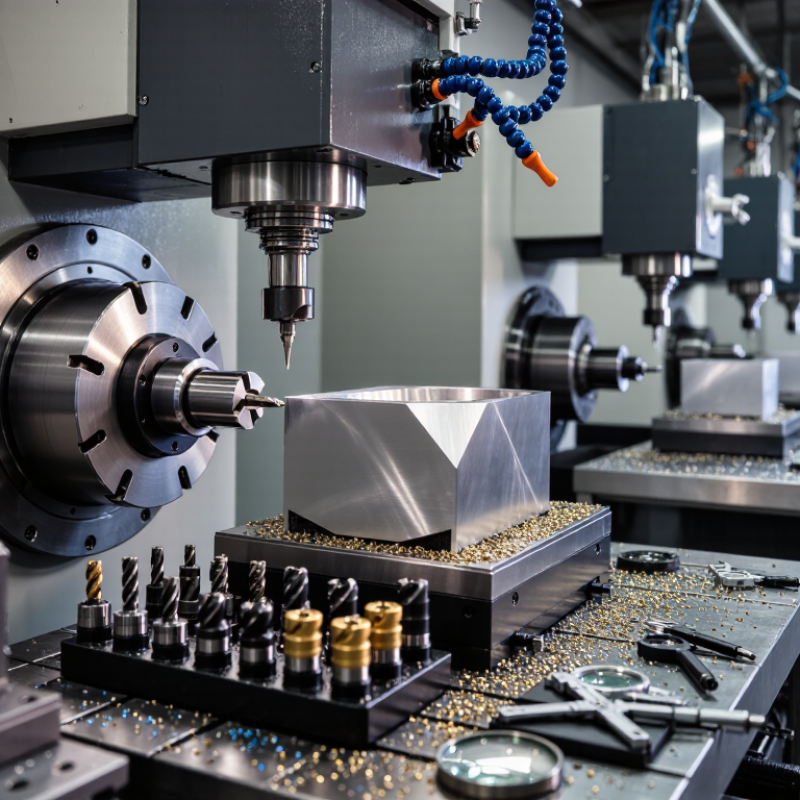
Before choosing a CNC cutting tool, define the job in measurable terms. Name the exact material and hardness, then record the operation: roughing, slotting, drilling, or finishing. A vague label like “stainless steel” is not enough; grade and work-hardening behavior can change the choice. Note the stock shape, allowance, target tolerance, surface finish, and production quantity. A 0.02 mm tolerance on a thin wall demands different planning from roughing a solid block.
Check the machine as carefully as the part. Record spindle speed and torque limits, tool reach, holder clearance, setup rigidity, coolant delivery, and how chips will leave the cut. A long tool may reach the pocket, but vibration can spoil the finish. I would verify the setup with a trial cut; the first estimate can be wrong. Small details matter.
Include operator exposure and fluid management in the requirements. NIOSH’s Criteria for a Recommended Standard: Occupational Exposure to Metalworking Fluids (1998) gives recommended exposure limits of 0.4 mg/m³ for thoracic particulate and 0.5 mg/m³ for total particulate, as time-weighted averages. These are U.S. recommendations, not universal legal limits or tool-selection thresholds. Still, they make coolant choice, mist control, and enclosure performance relevant to the process plan. Define these constraints before comparing tool geometry or coating.
Choosing the best CNC cutting tool starts with the workpiece, not the tool catalog. Match the cutting material to the workpiece’s hardness, heat, and abrasiveness. Carbide suits many production jobs because it holds its edge at higher cutting speeds. High-speed steel can be more forgiving at lower speeds or during interrupted cuts. No material wins every time.
Geometry matters just as much. Aluminum tends to benefit from sharp edges, polished flutes, and open chip spaces that reduce built-up material. Stainless steel often needs a strong, sharp edge and steady chip removal; rubbing can cause work hardening. For harder alloys, a tougher tool grade and conservative engagement may reduce edge chipping. Flute count, helix angle, and tool diameter also affect chip clearance and cutting forces. Small details count.
Tips: Check the tool maker’s cutting data, then adjust one variable at a time. Watch the chips: long, tangled ribbons or a changing surface finish can signal trouble. Confirm tool runout and workholding before blaming the geometry. A setup that looks correct on paper may still need adjustment on the machine.
Before selecting a cutter, confirm the machine can support its interface, diameter, length, and maximum speed. Check the holder taper, collet range, spindle torque, and available clearance. A long tool may reach the pocket, but it can also flex and leave chatter marks. Small checks matter.
Set cutting speed, feed per tooth, and engagement for the workpiece material and tool geometry.
For example, a 10 mm cutter at 150 m/min runs near 4,775 rpm; at 0.05 mm per tooth with four flutes, feed is about 955 mm/min. Treat this as a calculation example, not a universal recipe.
Verify the machine’s speed and feed limits, then adjust with a short test cut. I still find that chip shape and spindle sound can reveal problems the setup sheet missed.
Coolant delivery matters too: a nozzle that misses the cutting zone may leave heat and chips where they can damage the edge.
NIOSH’s 1998 Criteria for a Recommended Standard: Occupational Exposure to Metalworking Fluids gives recommended exposure limits of 0.4 mg/m³ for thoracic particulate mass or 0.5 mg/m³ for total particulate mass. That makes mist control part of machine and coolant-system planning, not an afterthought. Recheck the result.
Choosing a CNC cutting tool means comparing more than purchase price. Track metal-removal rate, surface finish, tool changes, and cost per acceptable part. A tool that cuts faster may still lose if it creates chatter or rejects. In a controlled test, record spindle speed, feed, depth of cut, material, and coolant use; change one variable at a time. Small details matter.
Tips: Use a consistent end-of-life measure. ISO 3685:1993 describes tool-life testing for single-point turning tools and includes 0.3 mm average flank wear as a commonly used criterion for carbide tools. Compare tools under the same conditions, then divide tooling and changeover costs by the number of good parts produced. Keep the test sheet. Operator notes about a rough edge or a sudden burr can explain what a spreadsheet misses.
Service life is not just minutes in the cut. A longer-lasting insert can reduce interruptions, but only if it holds size and finish across the run. Check wear at set intervals with a loupe or microscope, and note when the first unacceptable surface appears. One caveat: shop-floor results may differ from a controlled test. Heat, chip evacuation, and setup rigidity all shift tool life, sometimes more than expected.
| Tool Material | Best-Suited Materials | Typical Cutting-Speed Range | Wear Resistance | Relative Tool Cost | Service-Life Potential | Main Advantages | Key Limitations |
|---|---|---|---|---|---|---|---|
| High-Speed Steel (HSS) | Low-carbon and mild steels, softer alloys, and general-purpose work where toughness is important. | About 20–40 m/min (65–130 ft/min) when cutting mild steel. | Low to moderate; generally lower hot-hardness than carbide. | Low; reference cost index: 1. | Moderate at conservative speeds; may lose hardness more quickly as cutting temperature rises. | Tough, relatively inexpensive, and suitable for interrupted cuts and less rigid setups. | Requires lower cutting speeds and can produce longer cycle times in production work. |
| Cemented Carbide | Steels, stainless steels, cast irons, and many non-ferrous alloys; grade and coating should match the work material. | About 150–250 m/min (490–820 ft/min) for many mild-steel operations; use material-specific data. | High; coatings and carbide grades can improve resistance to abrasion, heat, or built-up edge. | Moderate; reference cost index: about 2–5. | Often high in stable, correctly programmed machining; cutting conditions strongly affect actual life. | Versatile, productive, and widely available in solid-tool and indexable forms. | Can chip or fracture with vibration, poor rigidity, or unsuitable feeds and engagement. |
| Ceramic | High-speed machining of cast iron and selected hardened steels or heat-resistant alloys, depending on grade. | Often about 500–1,000 m/min (1,640–3,280 ft/min) for suitable cast-iron operations. | Very high at elevated temperatures; performance depends on ceramic composition and cutting conditions. | High; reference cost index: about 3–8. | Can be productive at high speeds in continuous cuts, but may be short or inconsistent in interrupted cuts. | Retains hardness at high temperatures and can support very high cutting speeds. | Brittle compared with carbide; sensitive to impact, vibration, and sudden temperature changes. |
| Cubic Boron Nitride (CBN) | Hardened ferrous materials, commonly hardened steels around 45–70 HRC, and some hard cast irons. | About 100–250 m/min (330–820 ft/min) for many hardened-steel turning applications. | Very high against abrasion and heat in suitable hardened-steel applications. | Very high; reference cost index: about 8–25. | High in stable finishing cuts; edge life depends on hardness, depth of cut, and interruption. | Can machine hard ferrous materials and may reduce or eliminate grinding in suitable processes. | High initial cost; not usually economical for soft materials or unstable, heavy interrupted cuts. |
| Polycrystalline Diamond (PCD) | Aluminum alloys, copper, graphite, composites, and other non-ferrous or abrasive materials. | About 500–2,000 m/min (1,640–6,560 ft/min) for suitable aluminum operations. | Extremely high against abrasive wear in compatible non-ferrous materials. | Very high; reference cost index: about 10–30. | Very high in suitable applications, especially long production runs with abrasive non-ferrous materials. | Supports high speeds, long edge life, and excellent surface finish in appropriate materials. | Generally unsuitable for machining ferrous materials at elevated temperatures because of diamond’s chemical interaction with iron. |
Cutting speeds are indicative starting ranges for representative applications, not universal settings. Actual results depend on tool geometry and grade, workpiece condition, operation, coolant, machine rigidity, feed, and depth of cut. Relative cost indices are approximate comparisons per cutting edge, with HSS set to 1; prices vary by tool size and design. Follow the tool supplier’s recommendations and validate conditions with a controlled test cut.
After choosing a tool, test it on the actual material, not a convenient substitute. Run a short, repeatable cut and record spindle speed, feed rate, depth of cut, tool life, and surface finish. Check the edge under magnification; small chips or uneven wear can explain a rough wall or changing dimensions. Keep the workholding and coolant consistent. Change one setting at a time, or the result becomes hard to interpret.
Use measured results, not a single impressive cut. The 2024 Smart Manufacturing Survey by Deloitte and MAPI found that 92% of surveyed manufacturing executives expect smart manufacturing to drive competitiveness within three years. That supports using reliable process data, though it does not prove one tool or setup is best. Compare cost per acceptable part, including tool changes and scrap. Then adjust feed or speed in small steps, watching for vibration, heat discoloration, and chip shape. A neat chip is useful evidence, not a verdict. One trial can mislead. Repeat the test across several parts and note any variation. If the tool lasts longer but leaves a poor finish, the setup still needs work. A shop log is imperfect, too; operators may record results differently. Use clear units and the same inspection method.
Calculated starting spindle speeds for carbide tools at a constant cutting speed of 120 m/min.
Speeds are calculated using RPM = (cutting speed × 1,000) ÷ (π × tool diameter). Use them as starting points, then refine the setup through test cuts while checking chip formation, vibration, and surface finish. Actual limits depend on the tool, workpiece, machine, and toolholder.
Subscribe to our newsletter and receive the latest news and exclusive insights every month. No spam.
LabConsulting GmbH and LC LabService GmbH are Austrian companies which cooperate with over 600 manufacturers and offers a selection of more than 180,000 products and various laboratory product and service solutions for our Labcustomers.
Die LabConsulting GmbH und die LC LabService GmbH sind österreichische Unternehmen, die mit über 600 global verteilten Herstellern zusammenarbeiten und mit einer Auswahl von mehr als 180.000 Produkten und verschiedenen Laborprodukt- und Servicelösungen unseren Parnern im Labor anbieten.
INSTOCK CATALOGOur services
Our services