


What Are the 2026 Top Welding Flanged Pipe Types?
Choosing the right Welding Flanged Pipe in 2026 will require more than comparing catalog photographs or nominal sizes. Industrial buyers will examine pressure ratings, temperature cycles, corrosion exposure, welding access, and maintenance demands. The leading types may include weld neck, slip-on, socket weld, lap joint, blind, and long weld neck flanges. Each design leaves a different footprint on the piping system.
The details matter. John C. Lippold, a respected welding metallurgy expert and author, defines weldability this way: “Weldability is the capacity of a material to be welded under the fabrication conditions imposed into a specific, suitably designed structure and to perform satisfactorily in the intended service.” This principle keeps the discussion practical. A weld neck flange may reduce stress concentration near a high-pressure joint. A lap joint flange may simplify alignment during repeated disassembly. A socket weld flange can suit smaller process lines, but its crevice geometry deserves careful review.
This guide will compare the top Welding Flanged Pipe types expected to attract attention in 2026. It will connect design selection with ASME dimensional requirements, material traceability, weld procedure qualification, inspection, and field installation. A neat ranking can mislead. Service conditions often overturn a simple “best” choice. Even experienced teams can overlook thermal expansion, gasket seating, or limited welding clearance. That uncertainty deserves attention, not concealment. Readers will find practical comparisons, visible selection criteria, and a few uncomfortable questions about cost, reliability, and long-term maintenance.
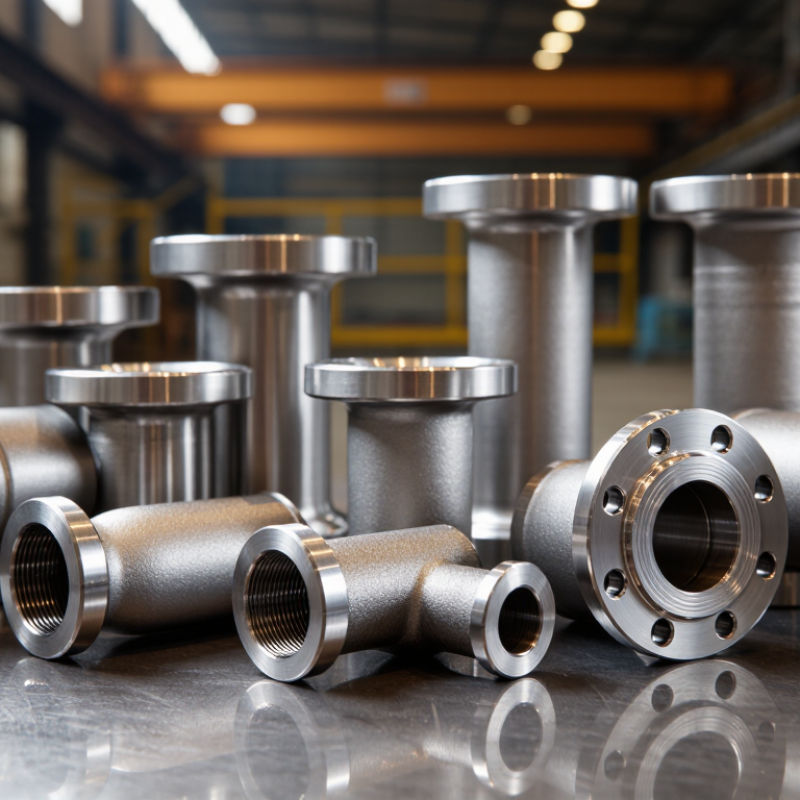
Definition and Role of Welding Flanged Pipes in Piping Systems
What Are the 2026 Top Welding Flanged Pipe Types?
A welding flanged pipe is a pipe fitted with a flange through a permanent welded joint. The flange creates a controlled connection between pipe sections, valves, pumps, and equipment nozzles. Bolts and gaskets then complete the pressure boundary. The weld carries structural loads, while the gasket limits leakage at the joint.
Common 2026 designs include weld-neck, slip-on, socket-weld, and blind flanges. Weld-neck flanges suit high-pressure lines, thermal cycling, and demanding process service. Their tapered hub transfers stress more smoothly into the pipe wall. Slip-on flanges are easier to align and often support general utility piping. Socket-weld flanges fit smaller, higher-pressure lines where internal bore control matters. Blind flanges close unused branches or permit future maintenance access.
Details decide performance. Short runs matter. A fabricator should check pipe schedule, flange facing, weld dimensions, gasket material, and bolt grade together. Misaligned faces can crush a gasket on one side. Excessive welding heat may distort the flange. Field experience shows that access for tightening is often underestimated during design. A drawing can look correct, yet a nearby support may block the wrench. It is also easy to over-specify every connection, increasing weight and installation cost without improving reliability. Engineers should verify pressure, temperature, corrosion allowance, inspection requirements, and applicable piping standards before selecting the final type.
What Are the 2026 Top Welding Flanged Pipe Types? - Definition and Role of Welding Flanged Pipes in Piping Systems
| Type | Definition and Connection Method | Typical Piping Role | Main Advantages | Limitations and Installation Considerations | Common Materials | Common Standards and Size Range |
|---|---|---|---|---|---|---|
| Weld Neck Flange | A long-tapered hub flange with a bevel bore. The pipe is butt-welded to the flange after the pipe end and flange bore are aligned. | High-integrity connections in process lines, pressure systems, high-temperature service, and critical equipment nozzles. | Excellent stress distribution, strong fatigue resistance, and low flow disturbance when the bore matches the pipe inside diameter. | Higher cost and weight than simpler flange types; requires qualified butt welding and accurate alignment. | Carbon steel, stainless steel, low-alloy steel, duplex stainless steel, nickel alloys, and other engineered alloys. | ASME B16.5 generally covers NPS 1/2 through NPS 24; ASME B16.47 covers larger nominal sizes, commonly NPS 26 through NPS 60. |
| Slip-On Flange | A flat-hub flange that slips over the pipe. It is normally attached with fillet welds on the outside and, where specified, on the inside. | General-purpose utility, water, air, and moderate-pressure process piping where installation economy is important. | Easy alignment, relatively low material cost, and simpler field fabrication than a weld neck design. | Lower fatigue and pressure-cycle resistance than a weld neck flange; weld quality and pipe insertion depth must be controlled. | Carbon steel, stainless steel, alloy steel, and selected nonferrous alloys. | ASME B16.5 for NPS 1/2–24 and ASME B16.47 for larger sizes; pressure classes commonly include 150, 300, 600, and higher where permitted by the standard. |
| Socket Weld Flange | A flange with a socket recess. The pipe is inserted into the socket and attached with a fillet weld around the outside. | Small-bore, high-pressure utility and process piping where compact dimensions and good alignment are required. | Accurate pipe positioning, compact construction, and no internal weld protrusion when correctly installed. | Generally used for smaller nominal pipe sizes; a specified internal gap is required before welding to accommodate thermal expansion. | Carbon steel, stainless steel, alloy steel, and nickel-based alloys. | ASME B16.5; commonly selected for smaller sizes and pressure classes such as 150, 300, 600, and 1500, subject to design requirements. |
| Blind Flange | A solid flange without a center bore. It is bolted to a mating flange to close the end of a pipe, valve, vessel nozzle, or branch connection. | Line isolation, pressure testing, future expansion points, equipment maintenance, and temporary or permanent pipe termination. | Provides positive closure and can be removed for inspection, cleaning, or system extension. | Bolt loads and flange thickness must be adequate for the design pressure; it does not provide a flow path. | Carbon steel, stainless steel, alloy steel, duplex stainless steel, and nickel alloys. | ASME B16.5 for NPS 1/2–24 and ASME B16.47 for larger sizes; pressure classes can range from 150 to 2500 depending on size and material. |
| Lap Joint Flange with Stub End | A loose flange used with a separate stub end. The stub end is butt-welded to the pipe, while the flange can rotate freely around the joint. | Corrosion-resistant piping, frequent dismantling points, lined systems, and applications requiring easy bolt-hole alignment. | Reduces alignment difficulty, limits exposure of expensive alloy material, and simplifies repeated disassembly. | The loose flange is not suitable for every high-load application; the stub end and gasket face must be correctly matched. | Carbon steel backing flanges with stainless steel, duplex, nickel alloy, or other corrosion-resistant stub ends. | ASME B16.5; commonly used where the selected stub-end dimensions and flange facing are compatible with the piping specification. |
| Integral Flange | A flange formed as one continuous piece with a pipe, fitting, or equipment component, or engineered to act structurally as an integral connection. | Specialized high-pressure, high-temperature, or heavily loaded connections where structural continuity is essential. | Strong load transfer and reduced reliance on a separate flange-to-pipe attachment. | Usually more difficult and expensive to manufacture; dimensions may be governed by equipment or project-specific engineering. | Forged carbon steel, alloy steel, stainless steel, and high-performance alloys. | Designed in accordance with applicable piping, pressure-vessel, equipment, and project specifications; dimensions may not be limited to one standard flange series. |
| Threaded Flange | A flange with an internal thread that engages a threaded pipe. It normally does not require welding at the pipe connection. | Special service, low-temperature, or locations where welding is restricted and the piping size is relatively small. | No field welding is needed at the pipe joint, reducing hot-work requirements and installation time. | Not normally preferred for severe cyclic, high-temperature, or highly corrosive service because threads may create leakage and stress-concentration concerns. | Carbon steel, stainless steel, and alloy steel, subject to service compatibility. | ASME B16.5; thread form and pipe compatibility must be verified against the applicable piping specification. |
Newsletter
Subscribe to our newsletter and receive the latest news and exclusive insights every month. No spam.

LabConsulting GmbH and LC LabService GmbH are Austrian companies which cooperate with over 600 manufacturers and offers a selection of more than 180,000 products and various laboratory product and service solutions for our Labcustomers.
Die LabConsulting GmbH und die LC LabService GmbH sind österreichische Unternehmen, die mit über 600 global verteilten Herstellern zusammenarbeiten und mit einer Auswahl von mehr als 180.000 Produkten und verschiedenen Laborprodukt- und Servicelösungen unseren Parnern im Labor anbieten.
INSTOCK CATALOG


Our services
Our services

