Explore cutting-edge articles on laboratory products, industry innovations, and research trends with Lab Consulting.
Choosing the right roll thread machine in 2026 requires more than comparing prices and motor power. Global buyers must examine thread size, material compatibility, production volume, automation level, and after-sales support. A compact machine may suit a small workshop, while a high-output model needs stable power, trained operators, and reliable tooling.
Details matter. This guide introduces major machine types for different manufacturing conditions. It considers flat-die, cylindrical-die, planetary, and CNC-controlled designs. Each type forms threads differently and serves specific workpieces. Steel fasteners, automotive parts, construction hardware, and precision components may require different pressure settings and die configurations. Practical selection should also include cycle time, changeover effort, dimensional accuracy, safety guarding, and spare-part availability.
Specifications can look impressive on paper. Real performance may differ. Buyers should request sample testing, inspection records, and clear warranty terms before placing an order. Supplier experience also matters, especially when installation, operator training, or remote troubleshooting is required across borders. Certifications should be checked against the destination market, not accepted blindly. No guide removes every uncertainty. Even experienced buyers can overlook shipping damage, voltage differences, or local maintenance limits.
This overview provides a practical starting point for evaluating the best roll thread machine types for global purchasing decisions. It combines technical considerations with real factory concerns, helping readers compare machines with greater confidence. Fit comes first. Reliability matters more than advertising.
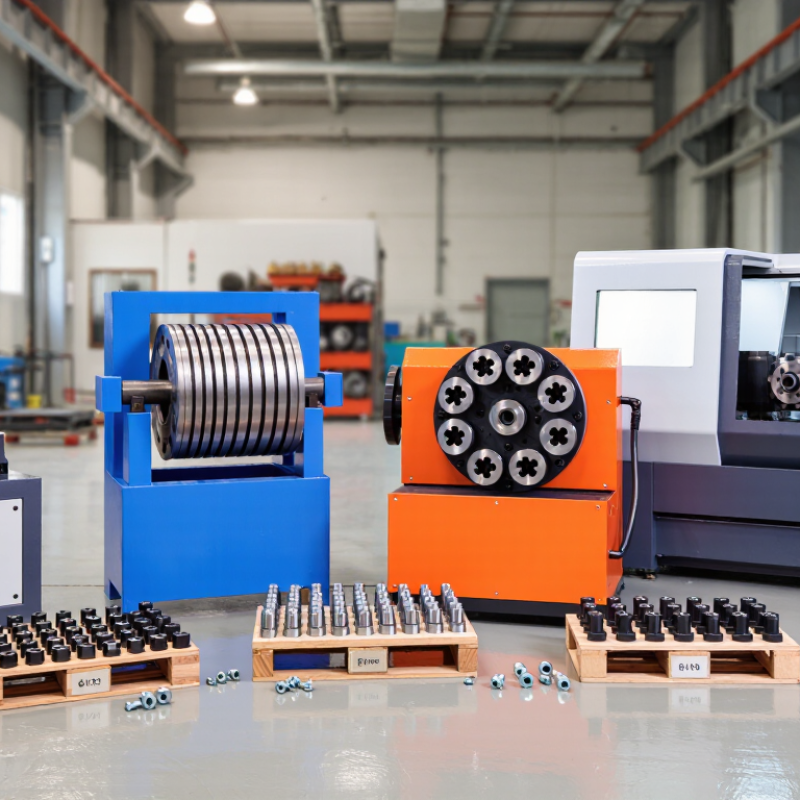
A roll thread machine forms threads by pressing hardened dies against a rotating metal blank. Unlike cutting, it displaces material instead of removing it. The blank rotates between two or more dies, while pressure pushes metal into the thread profile. The process can improve grain flow, surface hardness, and thread strength when speed, lubrication, and blank diameter are correctly matched. ISO 898-1 remains a useful reference when buyers evaluate mechanical properties for fastener applications.
The machine type matters.
Flat-die models suit high-volume production and simple cylindrical parts. Planetary machines handle continuous output with compact layouts. Two-die cylindrical systems offer flexibility for different diameters and shorter production runs. A technician should check die alignment, spindle speed, feeding accuracy, and cooling before judging capacity. Small errors leave visible double marks.
Industry data gives useful context. The World Steel Association reported 1.892 billion tonnes of crude steel production worldwide in 2023, showing the scale of the metalworking supply base. Grand View Research has also identified automation and precision forming as major drivers in the global metal forming equipment market. These figures do not guarantee machine performance. They only show strong industrial demand.
In practice, rolled threads may reduce scrap because chips are not produced. Yet this advantage is sometimes overstated. Hard alloys, poor lubrication, or incorrect preform sizing can cause die wear and unstable results. Buyers should request sample trials, dimensional reports, and cycle-time records before placing an order. A polished brochure is not proof.
Flat-die roll thread machines suit small and medium fasteners. They use two reciprocating dies to form threads quickly. These machines are practical for bolts, studs, and short threaded parts. Operators can change dies without complex setup. However, die alignment needs regular inspection. A small offset may create uneven crests or damaged ends.
Cylindrical-die machines support continuous production with rotating dies. Through-feed models work well for long screws, rods, and repeated parts. The material enters one side and exits the other. In-feed models hold each workpiece between rotating dies. They are better for short parts requiring controlled thread length. Production teams should check diameter, hardness, and blank preparation before selecting either type.
Planetary machines can process high volumes with stable feeding. They often suit automotive fasteners and other standardized components. CNC-controlled models offer better adjustment for mixed batches. They can store settings for pitch, length, and forming pressure. Useful, but not effortless. Skilled technicians still verify trial pieces with thread gauges and dimensional tools. From practical shop-floor evaluations, speed alone is a poor buying standard. Die life, coolant control, noise, floor space, and maintenance access also affect real operating costs. A machine that looks efficient may perform poorly with inconsistent blanks. Global buyers should request test reports, service details, and clear tolerance data before placing an order.
2026 Best Roll Thread Machine Types for Global Buyers
When comparing thread rolling equipment, start with measurable specifications, not catalog claims. Check the maximum rolling diameter, pitch range, die width, rolling force, spindle speed, and workpiece length. A machine rated for 120 kN may still perform poorly on hardened steel if its die support lacks rigidity. ISO 230-2 provides a useful framework for checking positioning accuracy and repeatability. Also review cycle time, hydraulic pressure stability, motor power, and tool-change access. These details affect output more than a dramatic speed figure.
Energy deserves closer attention. The International Energy Agency’s Energy Efficiency 2024 report states that industry uses roughly 37% of global final energy. Therefore, buyers should compare motor efficiency, idle consumption, and average power per finished part. The machine’s control system should record force curves, alarms, and dimensional results. Digital records improve traceability, but they do not replace skilled inspection. My experience suggests that buyers often overvalue maximum speed. That can be a costly mistake. A slower machine may produce steadier threads and fewer rejected parts.
Tips: Request sample trials using your actual material, diameter, and pitch. Measure thread angle, pitch diameter, surface finish, and repeatability across several batches. Ask for noise, vibration, maintenance, and compressed-air data. ISO 9001-based suppliers should provide controlled inspection records. Still, paperwork can look perfect while operator training remains weak. Verify both. Test before ordering.
| Machine Type | Die Arrangement | Typical Workpiece Diameter | Typical Thread Length | Typical Rolling Force | Typical Production Rate | Best-Suited Applications | Key Advantages | Main Limitations |
|---|---|---|---|---|---|---|---|---|
| Flat-Die Thread Rolling Machine | Two reciprocating flat dies | Approximately 2–30 mm | Approximately 5–120 mm | Approximately 50–400 kN | About 30–250 pieces/min, depending on part geometry | Screws, studs, small shafts, fasteners and high-volume small parts | Low tooling cost; compact layout; high output for small parts; simple loading and unloading | Limited suitability for large diameters, long threads and complex profiles |
| Two-Roll Cylindrical Thread Rolling Machine | Two parallel cylindrical dies | Approximately 3–80 mm | Approximately 10–250 mm | Approximately 100–1,200 kN | About 10–80 pieces/min, depending on diameter and thread length | Automotive shafts, threaded bars, fittings, pins and medium-to-large fasteners | Flexible diameter range; strong thread profile; suitable for through-feed and in-feed rolling | Higher die cost; requires accurate workpiece positioning and stable material preparation |
| Three-Roll Planetary Thread Rolling Machine | One fixed roll with two planetary rolls, or three coordinated rolls | Approximately 3–30 mm | Typically through-feed; effective lengths commonly above 100 mm | Approximately 150–1,000 kN | About 60–300 pieces/min for suitable continuous-feed parts | Long threaded rods, continuous production of bolts, tubes and narrow shafts | Very high throughput; reduced axial movement; efficient for long, continuous threads | Less suitable for short irregular parts; tooling and setup are more specialized |
| Three-Roll In-Feed Thread Rolling Machine | Three radial rolls positioned around the workpiece | Approximately 5–100 mm | Approximately 10–200 mm | Approximately 300–2,000 kN | About 5–40 pieces/min, depending on part size and forming depth | Precision shafts, bearing components, worm-like profiles and short threaded parts | Good concentricity; strong radial support; suitable for larger diameters and short threads | Slower than continuous-feed systems; higher power and tooling requirements |
| Rotary-Head Thread Rolling Machine | Multiple rolling dies mounted in a rotating head | Approximately 3–50 mm | Approximately 5–150 mm | Approximately 100–800 kN | About 20–120 pieces/min, depending on loading method | Precision fasteners, medical components, fittings and parts requiring controlled axial positioning | Good control of thread location; compact die head; suitable for automated lines | More complex maintenance; die-head balance and alignment are critical |
| CNC Servo Thread Rolling Machine | Two or three powered rolls with CNC-controlled axes | Approximately 2–100 mm, subject to machine capacity | Approximately 5–300 mm | Approximately 100–2,000 kN | About 5–100 pieces/min, depending on process complexity | Mixed production, precision components, variable pitches and digitally controlled manufacturing cells | Fast recipe changes; repeatable positioning; process monitoring; easy integration with automation | Higher purchase price; requires trained operators and reliable electrical maintenance |
| Hydraulic Heavy-Duty Thread Rolling Machine | Two or three rolls driven by hydraulic forming force | Approximately 20–200 mm | Approximately 30–500 mm | Approximately 800–5,000 kN | About 1–15 pieces/min, depending on size and material | Large-diameter studs, structural components, oil and gas fittings, heavy shafts and special profiles | High forming capacity; suitable for large workpieces and difficult-to-form materials | Large footprint; slower cycle time; higher hydraulic maintenance and energy demand |
Choosing a roll thread machine begins with the part, not the catalog. Measure thread diameter, pitch, length, material hardness, and required accuracy. Through-feed machines suit long, repeated parts. In-feed machines handle shoulders, short lengths, and controlled thread positions. For mixed production, a programmable model may reduce changeover time. It usually costs more.
Check forming force before comparing cycle speeds. Hardened steel needs stronger tooling and stable hydraulic pressure. Softer alloys may require careful pressure control to prevent surface tearing. Ask for sample trials using your actual material and drawings. Inspect thread crests under magnification. Small defects can cause serious assembly problems.
Think beyond production output. Confirm electrical requirements, guarding, noise limits, operator training, and documentation for the destination market. Local service access matters. So do spare rollers, sensors, and seals. I once saw a buyer select a fast machine without checking floor loading. Installation became expensive and delayed production. That mistake is easy to repeat. Request test data, maintenance intervals, tolerance records, and a clear warranty scope. Verify whether the controls support your factory’s language and data systems. Leave space around the machine for tooling changes and safe inspection. A perfect specification can still fail when operators lack practical training.
2026 Best Roll Thread Machine Types for Global Buyers
Installation, Operation, and Maintenance Considerations for Buyers
Choosing between flat-die, cylindrical, and planetary roll thread machines depends on product size and production volume. Installation starts with a rigid, level foundation that prevents vibration during forming. Measure the floor carefully. Small alignment errors can affect thread accuracy and die life. Buyers should also confirm voltage, guarding, ventilation, and local electrical requirements before shipment. A qualified technician should complete commissioning and record test results.
During operation, trained staff must match the dies, material hardness, feed rate, and forming pressure. Operators should inspect thread samples frequently, especially during the first production hours. Excessive pressure may damage dies or deform the workpiece. Insufficient pressure creates incomplete threads. Real installations are rarely perfect; material batches can behave differently, so settings may need adjustment.
Tips: Keep a daily inspection log. Clean chips from die holders after each shift. Check lubrication levels, hydraulic hoses, bearings, and emergency stops weekly. Replace worn dies before quality declines. Store critical spare parts in dry, labeled containers. Remote buyers should request maintenance manuals, wiring diagrams, training records, and acceptance-test data. One practical improvement is often missed: leave safe clearance around the machine for cleaning and future repairs. This space may seem unnecessary at installation, but crowded layouts make maintenance slower and less safe.
Installation, operation, and maintenance considerations by machine type
The scores use a practical 1–5 buyer-assessment scale, where 5 indicates a more favorable condition. Flat-die machines generally offer simpler installation and maintenance, two-roll cylindrical machines provide a balanced solution for precision and flexibility, and three-roll planetary machines can deliver high productivity but usually require more specialized setup and maintenance capability.
Subscribe to our newsletter and receive the latest news and exclusive insights every month. No spam.
LabConsulting GmbH and LC LabService GmbH are Austrian companies which cooperate with over 600 manufacturers and offers a selection of more than 180,000 products and various laboratory product and service solutions for our Labcustomers.
Die LabConsulting GmbH und die LC LabService GmbH sind österreichische Unternehmen, die mit über 600 global verteilten Herstellern zusammenarbeiten und mit einer Auswahl von mehr als 180.000 Produkten und verschiedenen Laborprodukt- und Servicelösungen unseren Parnern im Labor anbieten.
INSTOCK CATALOGOur services
Our services